The Process

What We Do

Everything we build starts with the client's engineering drawing and specification, and ends with a signed-off cabinet ready for dispatch. What happens in between is a six-stage process refined over thirty-five years to deliver precision, consistency, and quality that the world's leading audio brands depend on.

This page sets out how we work. Not to impress with jargon, but to show that every step has a reason, every material choice has a purpose, and every tolerance exists because the end product demands it.

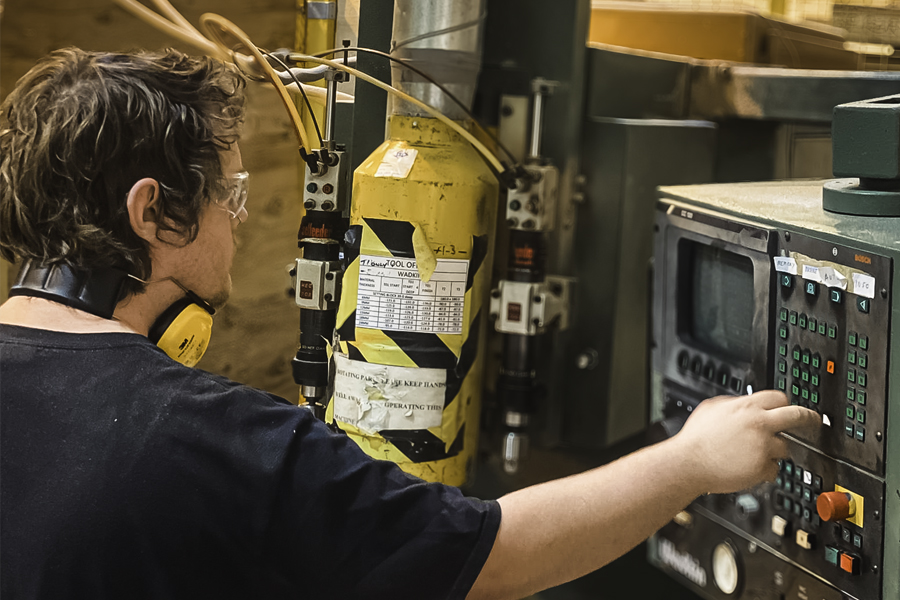
A CNC operator programming the router from an engineering drawing.
Stage 01

Design and Programming

Every cabinet we build starts with the client's engineering drawing. We do not originate the acoustic design; the client owns it. What we do is read the drawing closely, question anything that will not build cleanly, and resolve it with the client's design team before any material is committed. Our own design engineering experience is there to catch the problems that only appear on the workshop floor.

From the approved drawing we write a bespoke CNC programme for the cabinet. The programme defines every cut, route, pocket, rebate, and hole, and it is verified against the specification before a sheet is loaded. Test cuts prove it on a dry-assembled unit, and production does not begin until every tolerance is holding.
Engineering drawings and material specifications under review.
Stage 02

Material Selection

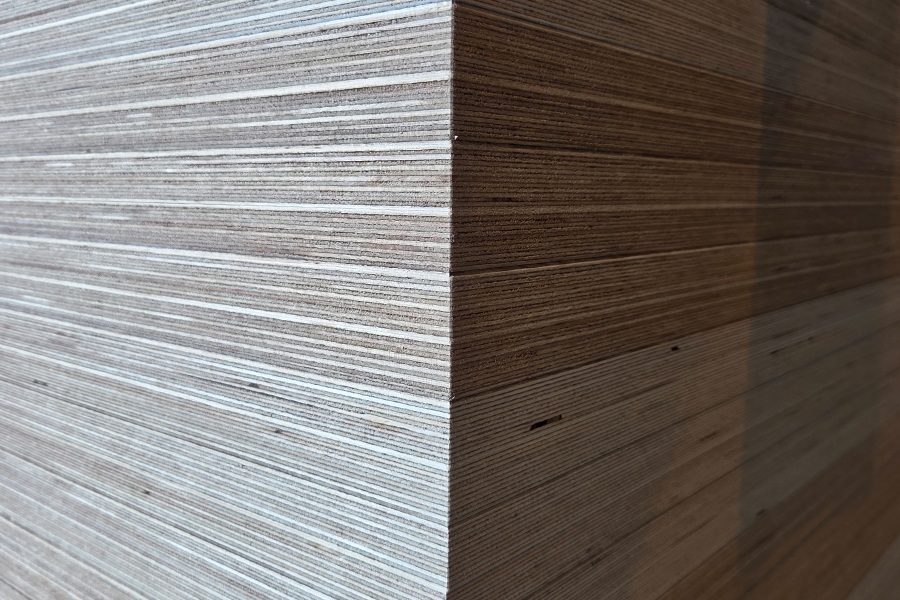
A cabinet is only as good as the sheet it is cut from. Baltic Birch is sourced for its density, consistency, and acoustic integrity. Each sheet is inspected, graded, and matched to the project specification before it enters the workshop.

Baltic Birch is not a compromise. It is a deliberate choice made for its uniform core structure, minimal void content, and predictable acoustic behaviour. Commodity plywood varies from sheet to sheet. Baltic Birch does not. When a client specifies a cabinet to perform within defined acoustic parameters, the material has to be as consistent as the machining. That starts with sourcing and inspection before a single sheet enters the workshop.

A craftsperson at work, machining timber to precise tolerances.
Stage 03

Machining and Shaping

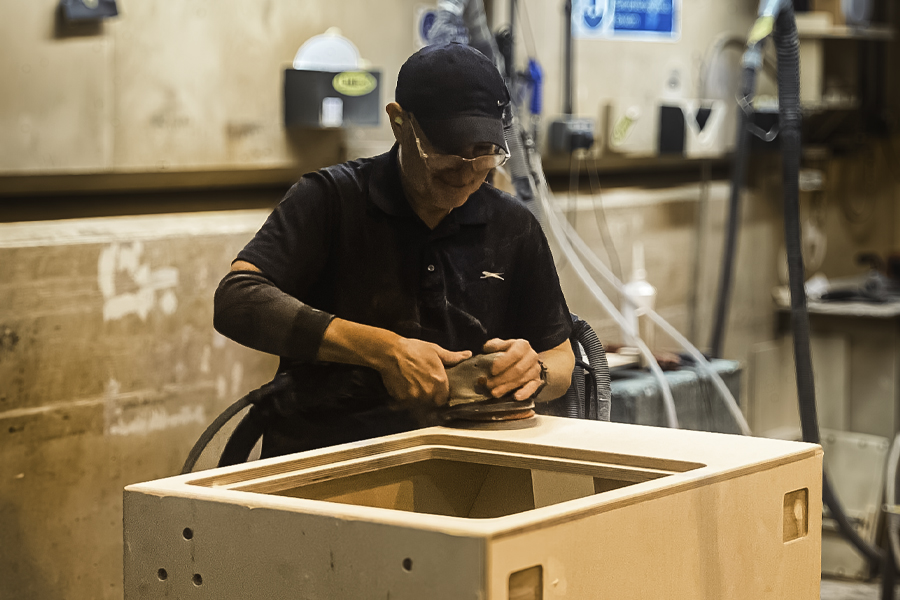
The CNC routers execute what the programming stage defined. Baltic Birch is cut, routed, and shaped to tolerances measured in fractions of a millimetre. The precision at this stage determines everything that follows. A cabinet that is even marginally out of specification at machining will never recover that accuracy downstream. This is where thirty-five years of process refinement shows.

Every toolpath is verified against the original engineering drawing before the first production run. Test cuts confirm dimensions, edge quality, and fit. The CNC machines are maintained to a schedule that prioritises accuracy over uptime, because a machine running fast and drifting by half a millimetre is worse than a machine running steady and holding tolerance.

Close-up of hand-built cabinet assembly in the Sarivale workshop.
Stage 04

Hand-Built Assembly

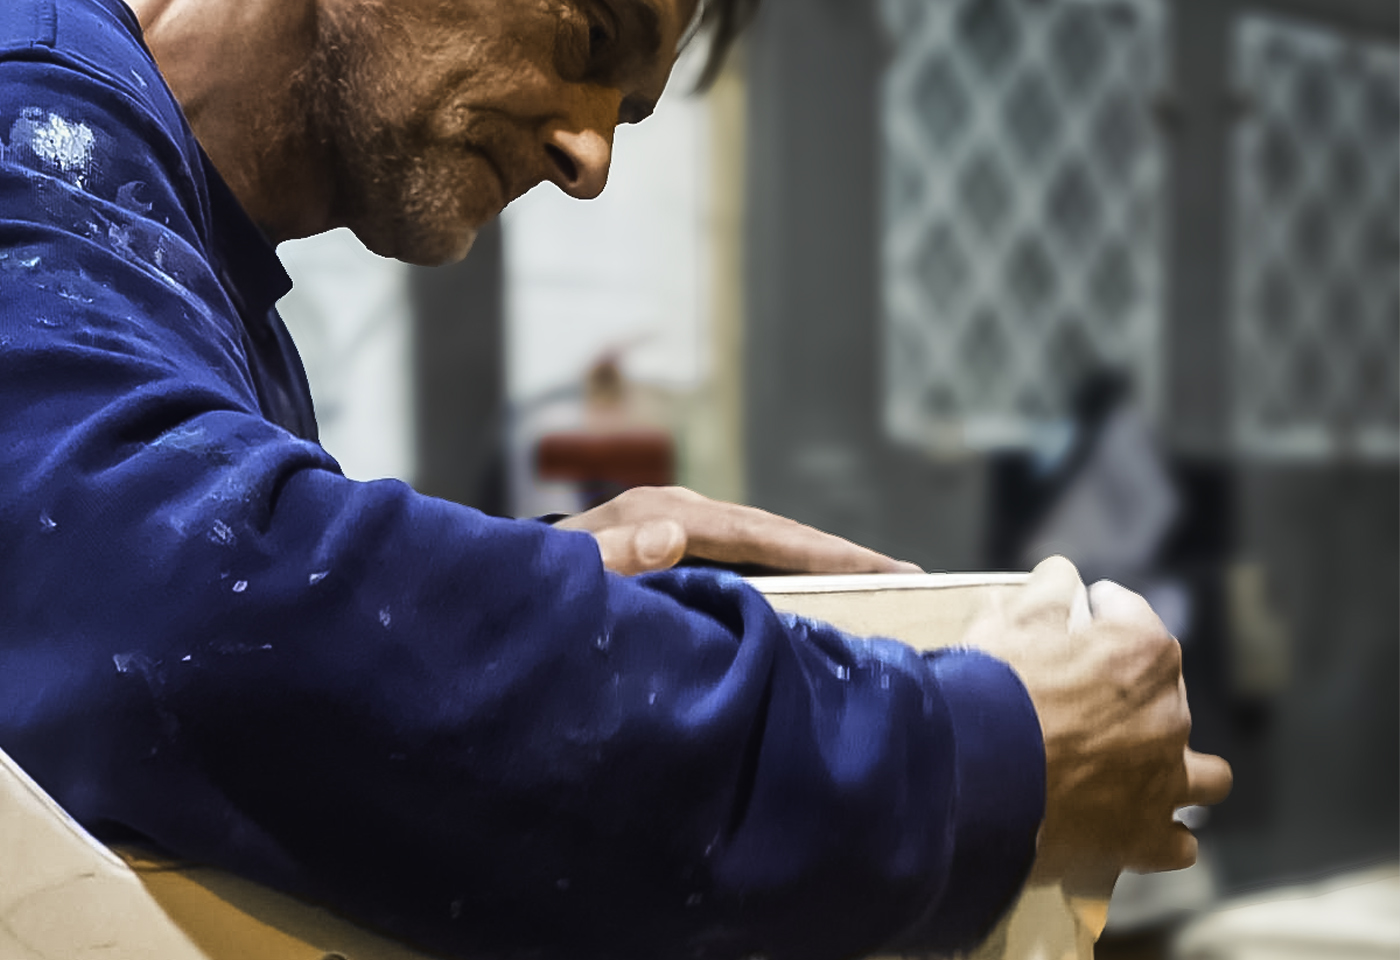
Machined panels become cabinets. Joints are glued, clamped, and set by hand, combining the accuracy of CNC machining with the judgement of experienced craftspeople. Internal bracing, driver mounting points, and port geometry are all assembled to the original specification. Every cabinet is checked against the engineering drawing before it moves forward.

There is a reason this stage is not automated. Assembly is where the judgement of an experienced craftsperson catches what a machine cannot: a panel that needs fractionally more pressure in the clamp, a joint that seats better from a different angle, a brace that needs a final check before the adhesive sets. Our assembly team has decades of combined experience, and that experience shows in every cabinet that leaves the bench.

Finishing materials being applied to a workshop surface.
Stage 05

Spray Shop

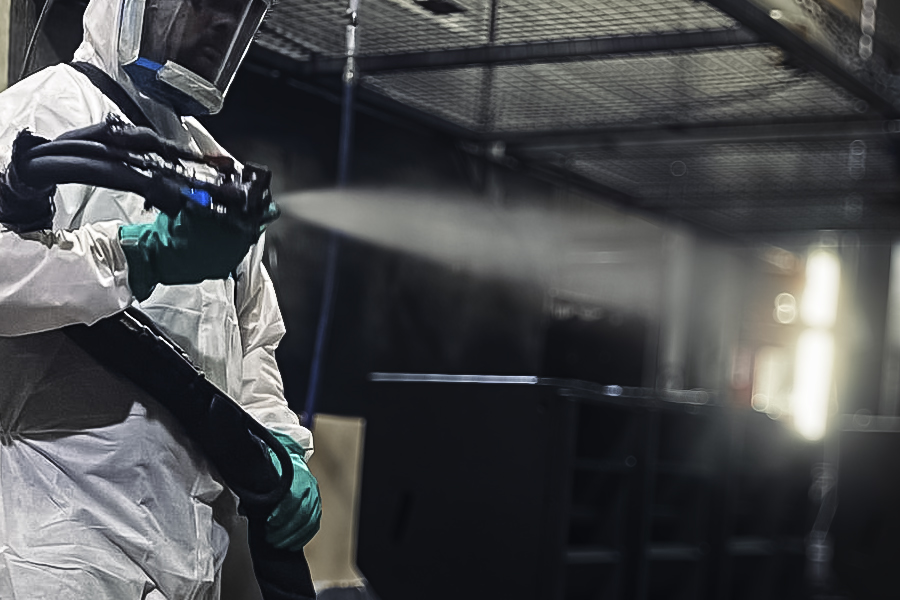
Coatings are selected to match the client's specification. The choice of primers, sealants, and topcoats is as considered as the choice of timber. Each cabinet receives multiple coats in a controlled spray environment.

The spray shop is not a cosmetic afterthought. The coating system affects acoustic damping, moisture resistance, durability under transport, and long-term appearance. A touring cabinet that will see the inside of a hundred flight cases needs a different finish from an installation cabinet that will sit in a fixed position for a decade. We specify the coating system to match the application, not the other way around.

Inspection of cabinet specifications against engineering drawings.
Stage 06

Final Inspection and Dispatch

Every cabinet is inspected against the original specification before it leaves the workshop. Dimensions, finish quality, hardware fitment, and cosmetic standards are all checked. Nothing leaves the workshop without sign-off.

Final inspection is not a formality. It is the last opportunity to catch anything that does not meet the standard, and it is taken seriously. Every cabinet is measured, visually inspected under controlled lighting, and assessed for fit and finish against the client's specification document. Every cabinet we make is then delivered personally, in our own lorry, by Trevor, who has been driving for Sarivale for over fifteen years.

Built to Last

Materials and Standards

Baltic Birch

Baltic Birch plywood is sourced specifically for its uniform core structure, minimal void content, and predictable acoustic properties. Unlike commodity plywood, which varies in density and consistency from sheet to sheet, Baltic Birch provides the stable, repeatable base that precision speaker cabinets demand. Every sheet is inspected on arrival and graded before it enters the production workflow.